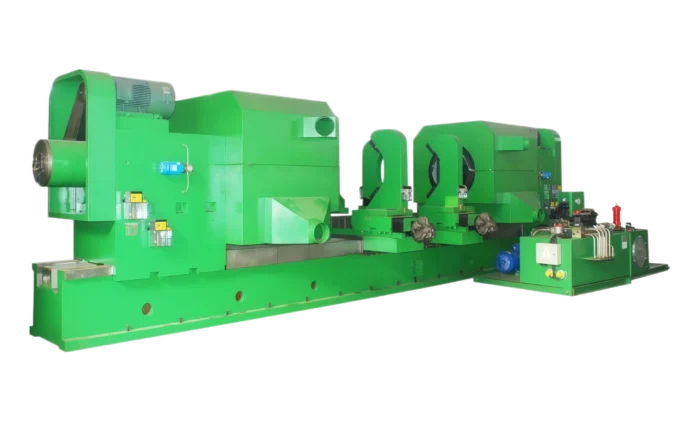
Carbon Electrode Processing Machinery
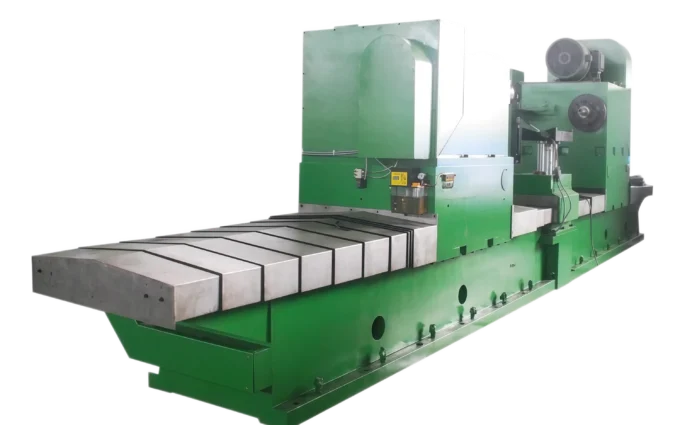
CGK-32 / CGK-75 CNC Electrode Double Thread Comb Processing Machine
The CGK-32 and CGK-75 cut the internal taper threads on both ends of a graphite electrode body from…
View SpecificationsThe CGK-32 and CGK-75 cut the internal taper threads on both ends of a graphite electrode body from…
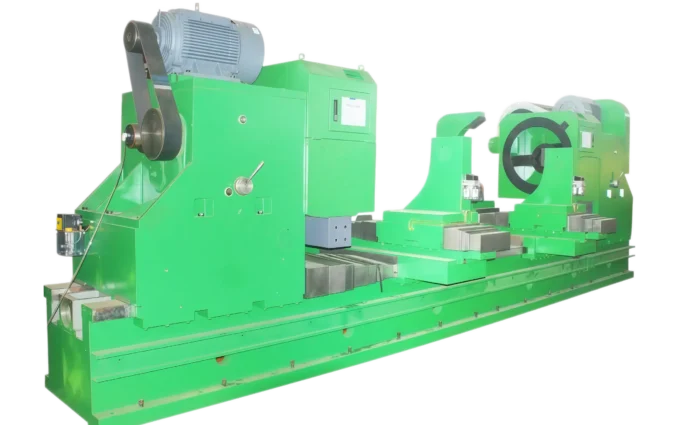
View SpecificationsThe CGK-31 and CGK-73 finish-turn graphite electrode bodies with multiple tools in a single CNC cycle.
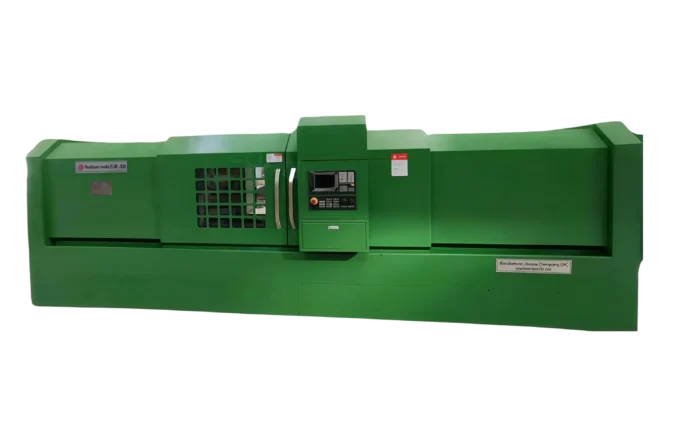
View SpecificationsThe CGK-19 and CGK-74 prepare graphite electrode bodies with parallel end faces and accurately centered holes before downstream…
View SpecificationsThe CGK-18 machines the internal taper thread that joins graphite electrode sections into a high-current furnace column.
View SpecificationsThe CGK·RZ·02 is built for carbon plants producing graphite electrode bodies — the current-carrying columns that thread into nipples to form the full electrode column in an electric arc furnace.
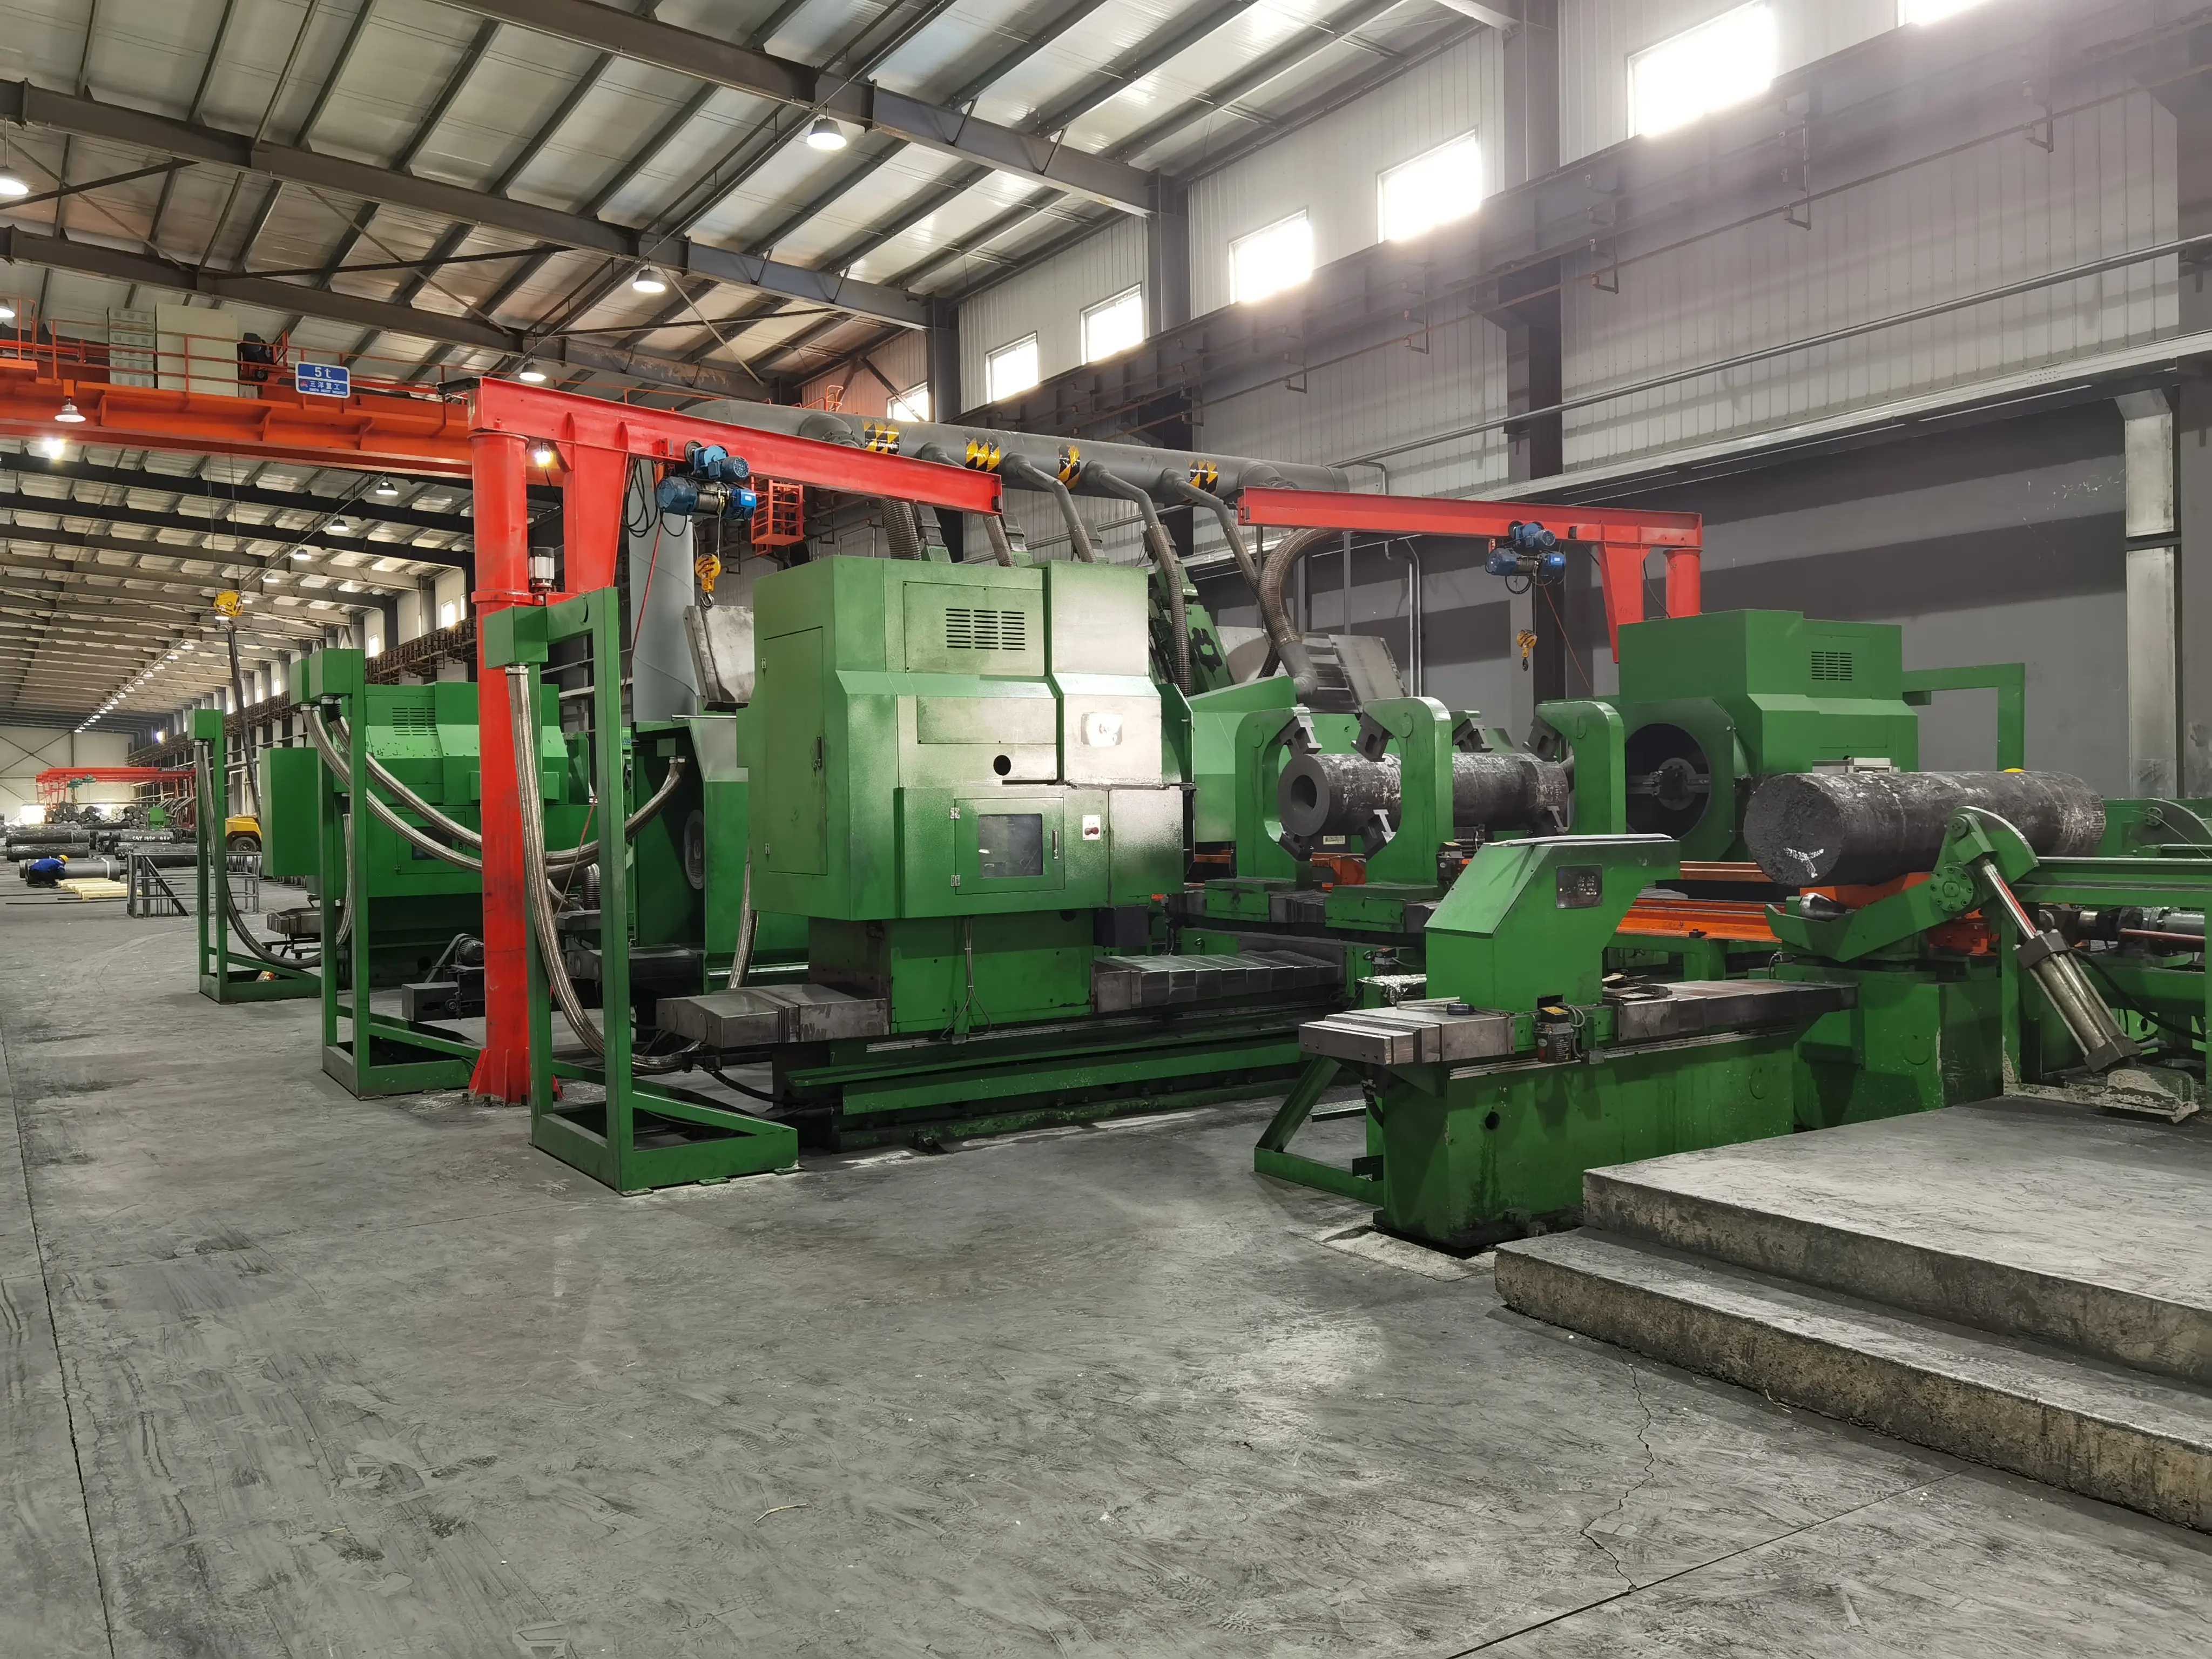
A graphite electrode body is the large-diameter column that carries the furnace current and threads into a nipple at each end. Its bore, outer diameter, thread profile and end-face flatness determine whether the electrode column runs straight and carries current without hot spots at the joints. Where plants run these operations on isolated machines with crane transfers between stations, the CGK·RZ·02 removes every manual hand-off and holds tolerance across the full sequence, because each station starts from a datum the previous station has already established.
Request a Line Layout →Five machining capabilities plus an automatic conveyor turn a row of standalone machines into one coordinated electrode-body line.
Bores the centre hole and scrapes both end faces in one clamping, establishing the common datum every downstream station works from.
Strips the oxidised skin and brings the full body length to finished diameter, holding cylindricity across long graphite columns.
Cuts the internal threads at both ends that mate with nipples, holding pitch error and thread-geometry accuracy on every body.
Finishes the end faces that seat against the nipple shoulder, controlling flatness and perpendicularity to protect joint sealing.
An overhead automatic conveyor transfers each electrode between stations, removing crane handling and floor-crew bottlenecks.
Electronic weighing, specific-resistance measurement, hole-bottom-circle machining and data printing can be added to match your quality protocol.
Against isolated electrode-body machines linked by crane handling, the CGK·RZ·02 wins on datum integrity, thread precision and lifecycle cost.
The line passes each body through boring, turning and threading in one datum chain, so re-clamping drift never compounds between stations.
Single-thread pitch error ≤0.015 mm, cumulative pitch error ≤0.025 / 150 mm and thread geometry within ±20′ — precision that controls joint resistance.
Full CNC on every station plus industrial PLC whole-line linkage lets the line run shifts with minimal floor presence.
Type I covers Φ300–Φ600 mm and Type II covers Φ450–Φ960 mm bodies — switch by calling a part program, not by retooling.
One automated line replaces isolated machines, cranes and manual inspection benches — cutting footprint, labour and cross-shift variability.
Optional upper-computer and remote-access architecture let supervisors track status, alarms and tool trends from the control room or offsite.
Main technical performance indicators from the factory datasheet.
| Parameter | Unit | Type I | Type II |
|---|---|---|---|
| Machined electrode diameter | mm | Φ300–Φ600 | Φ450–Φ960 |
| Machined electrode length | mm | 1500–3200 | 1600–3370 |
| Single-thread pitch error | mm | ≤0.015 | ≤0.015 |
| Cumulative thread pitch error | mm | ≤0.025 / 150 mm | ≤0.025 / 150 mm |
| Thread end-face perpendicularity | mm | ≤0.015 | ≤0.015 |
| Electrode end-face flatness | mm | ≤0.03 | ≤0.03 |
| Thread effective diameter error | mm | ≤0.10 | ≤0.10 |
| Thread hole effective diameter error | mm | 0–+0.08 | 0–+0.08 |
| Thread geometry accuracy | — | ±20′ | ±20′ |
| Coaxiality of thread and electrode center lines | mm | ≤0.15 | ≤0.15 |
| Outer-circle cylindricity error | mm | ≤0.07 | ≤0.07 |
| Cycle time per piece | min/pc | ≤5 | ≤5 |
Designed for baked and graphitised electrode bodies used in high-current submerged-arc and electric-arc furnace operations.
Send us your electrode diameter and length range, thread specification, Type I / Type II preference, daily throughput target, material grade, and workshop layout — including floor space, power supply and dust extraction capacity. Our engineering team will prepare a line layout with confirmed specifications, cycle-time estimate and quotation.
Request a Quote →