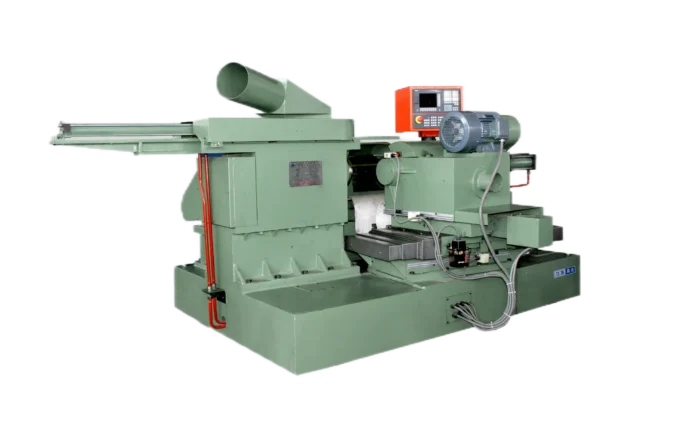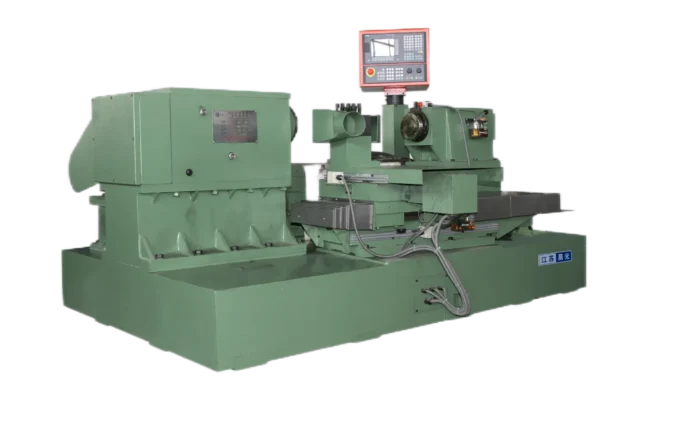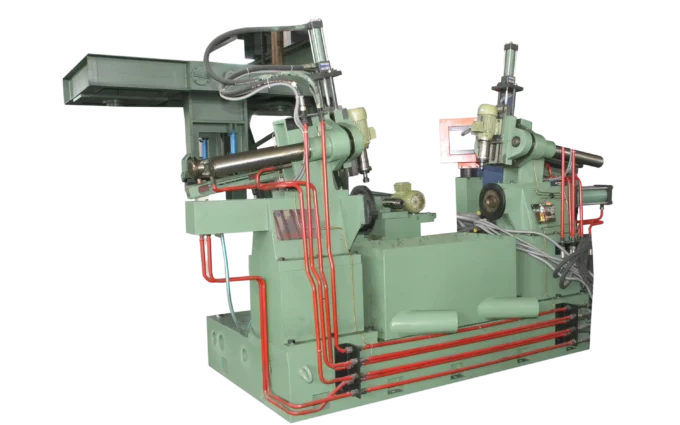
CGK-24 CNC Joint Double-End Scraping & Center-Hole Drilling Machine
Both Ends, One Setup, One Datum
The CGK-24 is built for plants machining graphite electrode nipples — preparing the end faces and centre hole that serve as the reference for every downstream threading operation.
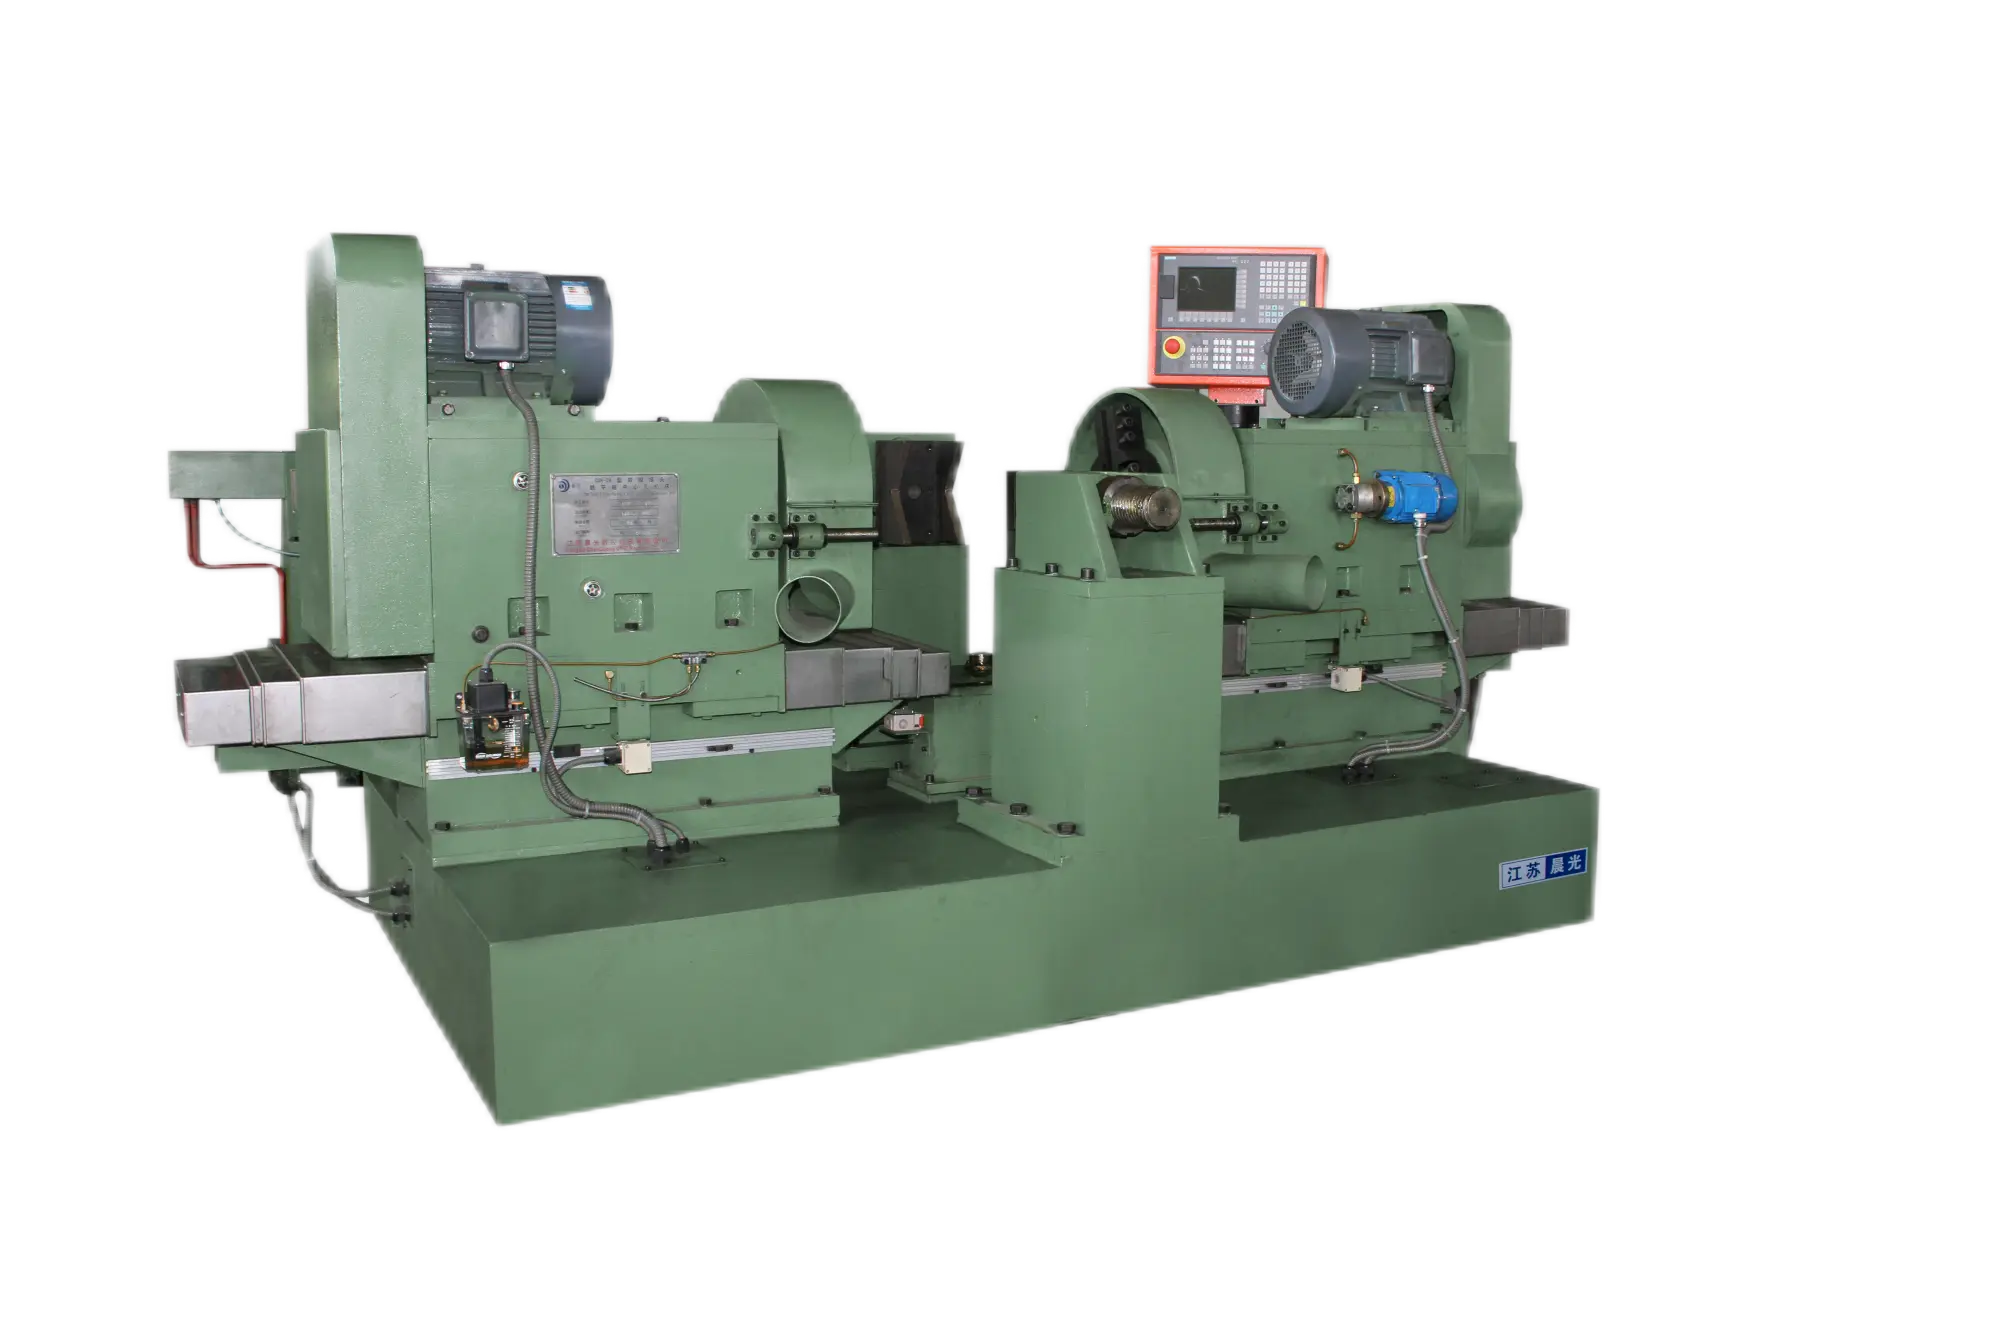
Every graphite electrode nipple needs a true centre hole and two square, parallel end faces before it can be threaded. Those surfaces are the datum the thread-combing and turning stations use to align the joint. The CGK-24 scrapes both end faces and drills the centre hole in one clamping, removing the re-clamping error that accumulates when facing and drilling are done on separate machines. The result is a nipple blank that enters the thread-combing station already centred and perpendicular, so the threads that follow run true to the axis.
Request a Quote →Key Features & Working Principle
Six capabilities that turn a two-machine facing-and-drilling job into one accurate setup.
Double-End Simultaneous Facing
Both nipple end faces are scraped in one clamping, so the two faces share the same axis and remain parallel to each other.
Centre-Hole Drilling
The centre hole is drilled from the same datum as the end faces, giving downstream threading stations a coaxial reference.
Full CNC Axis Control
Every motion axis is CNC controlled, eliminating mechanical transmission-chain error from face position and hole location.
Twin High-Torque Spindles
Two 7.5 kW main motors drive the facing and drilling heads through abrasive graphite without stalling or tearing the surface.
Rigid Cast Bed
A 6.9 tonne machine body absorbs cutting forces during double-end scraping, protecting surface finish and tool life.
Program-Driven Changeover
Different nipple diameters and lengths are handled by calling the stored part program — not by rebuilding fixtures or mechanical stops.
Why Choose the CGK-24
Against separate facing and drilling machines linked by manual handling, the CGK-24 wins on datum accuracy, handling damage and floor space.
Establishes the Whole Nipple Datum
The centre hole and both end faces are the references every downstream station uses; machining them together keeps them coaxial and square.
One Clamping Replaces Two Setups
Facing and drilling in one fixture removes a re-clamp, a crane move and the reference shift that often comes with it.
Tight Parallelism Control
End-face parallelism is held within 0.03 mm and overall length error within 0.1 mm — the squareness a furnace joint needs.
Wide Diameter Range
One machine covers Φ120–Φ431 mm nipple diameters and 177–635 mm lengths, so a nipple shop serves multiple electrode grades.
Less Handling Damage
Fewer clampings and transfers mean fewer chips on finished faces and fewer bent or dropped nipple blanks.
Compact Footprint
At 2460×1390×1400 mm, the machine replaces two standalone machines with one, freeing floor space in a busy nipple shop.
CGK-24 — Technical Data
Main technical performance indicators from the factory datasheet.
| Parameter | Unit | CGK-24 |
|---|---|---|
| Model | — | CGK-24 |
| Machined nipple diameter | mm | Φ120–Φ431 |
| Machined nipple length | mm | 177–635 |
| Main motor power | kW | 2 × 7.5 |
| Spindle speed | rpm | 230 |
| Pulse equivalent | mm/pulse | 0.001 |
| Length error | mm | 0.1 |
| Parallelism error | mm | 0.03 |
| Machine weight | t | 6.9 |
| Overall dimensions | mm | 2460×1390×1400 |
Materials & Industries Served
Designed for carbon plants preparing graphite electrode nipples before threading, turning and final inspection.
Frequently Asked Questions
What does the CGK-24 do?
What nipple sizes can the CGK-24 process?
What accuracy does the CGK-24 achieve?
Why machine both ends in one setup?
What control system does the CGK-24 use?
What information is needed for a quotation?
Configure a CGK-24 for Your Nipple Production
Send us your nipple diameter and length range, thread standard, taper ratio, pitch, electrode grade, daily throughput target, and workshop layout — including power supply and foundation requirements. Our engineering team will prepare a machine configuration with confirmed specifications and a quotation.
Request a Quote →