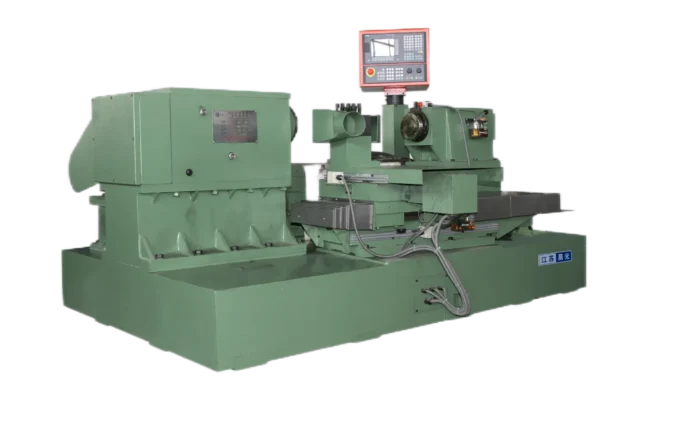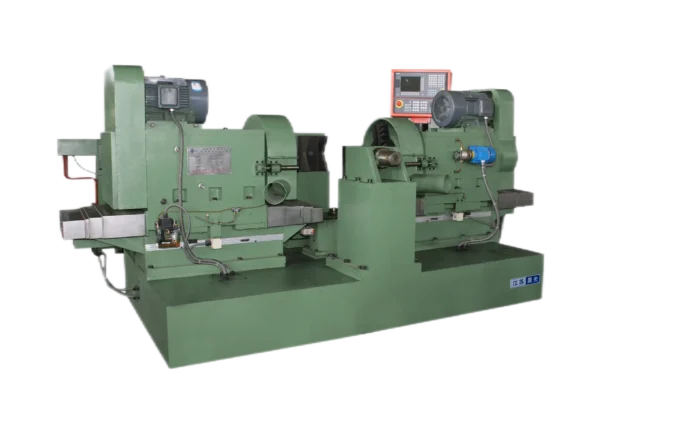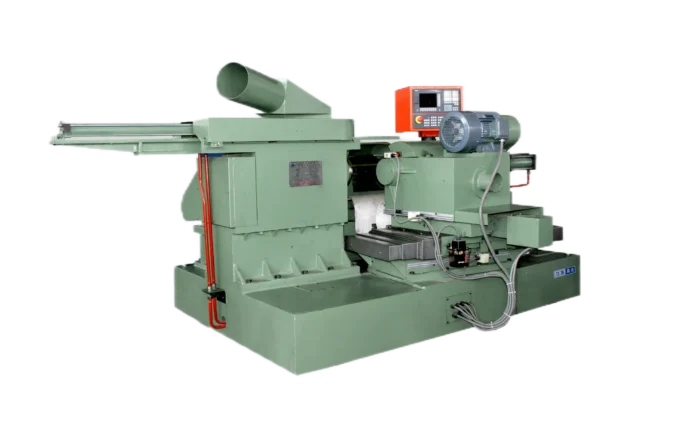
CGK-28 CNC Joint Milling Groove & Drilling Bolt Hole Machine
Slot, Bolt Hole, Both Ends, One Setup
The CGK-28 is built for plants machining graphite electrode nipples — adding the handling slot and bolt hole that sit alongside the threaded end of the connector.
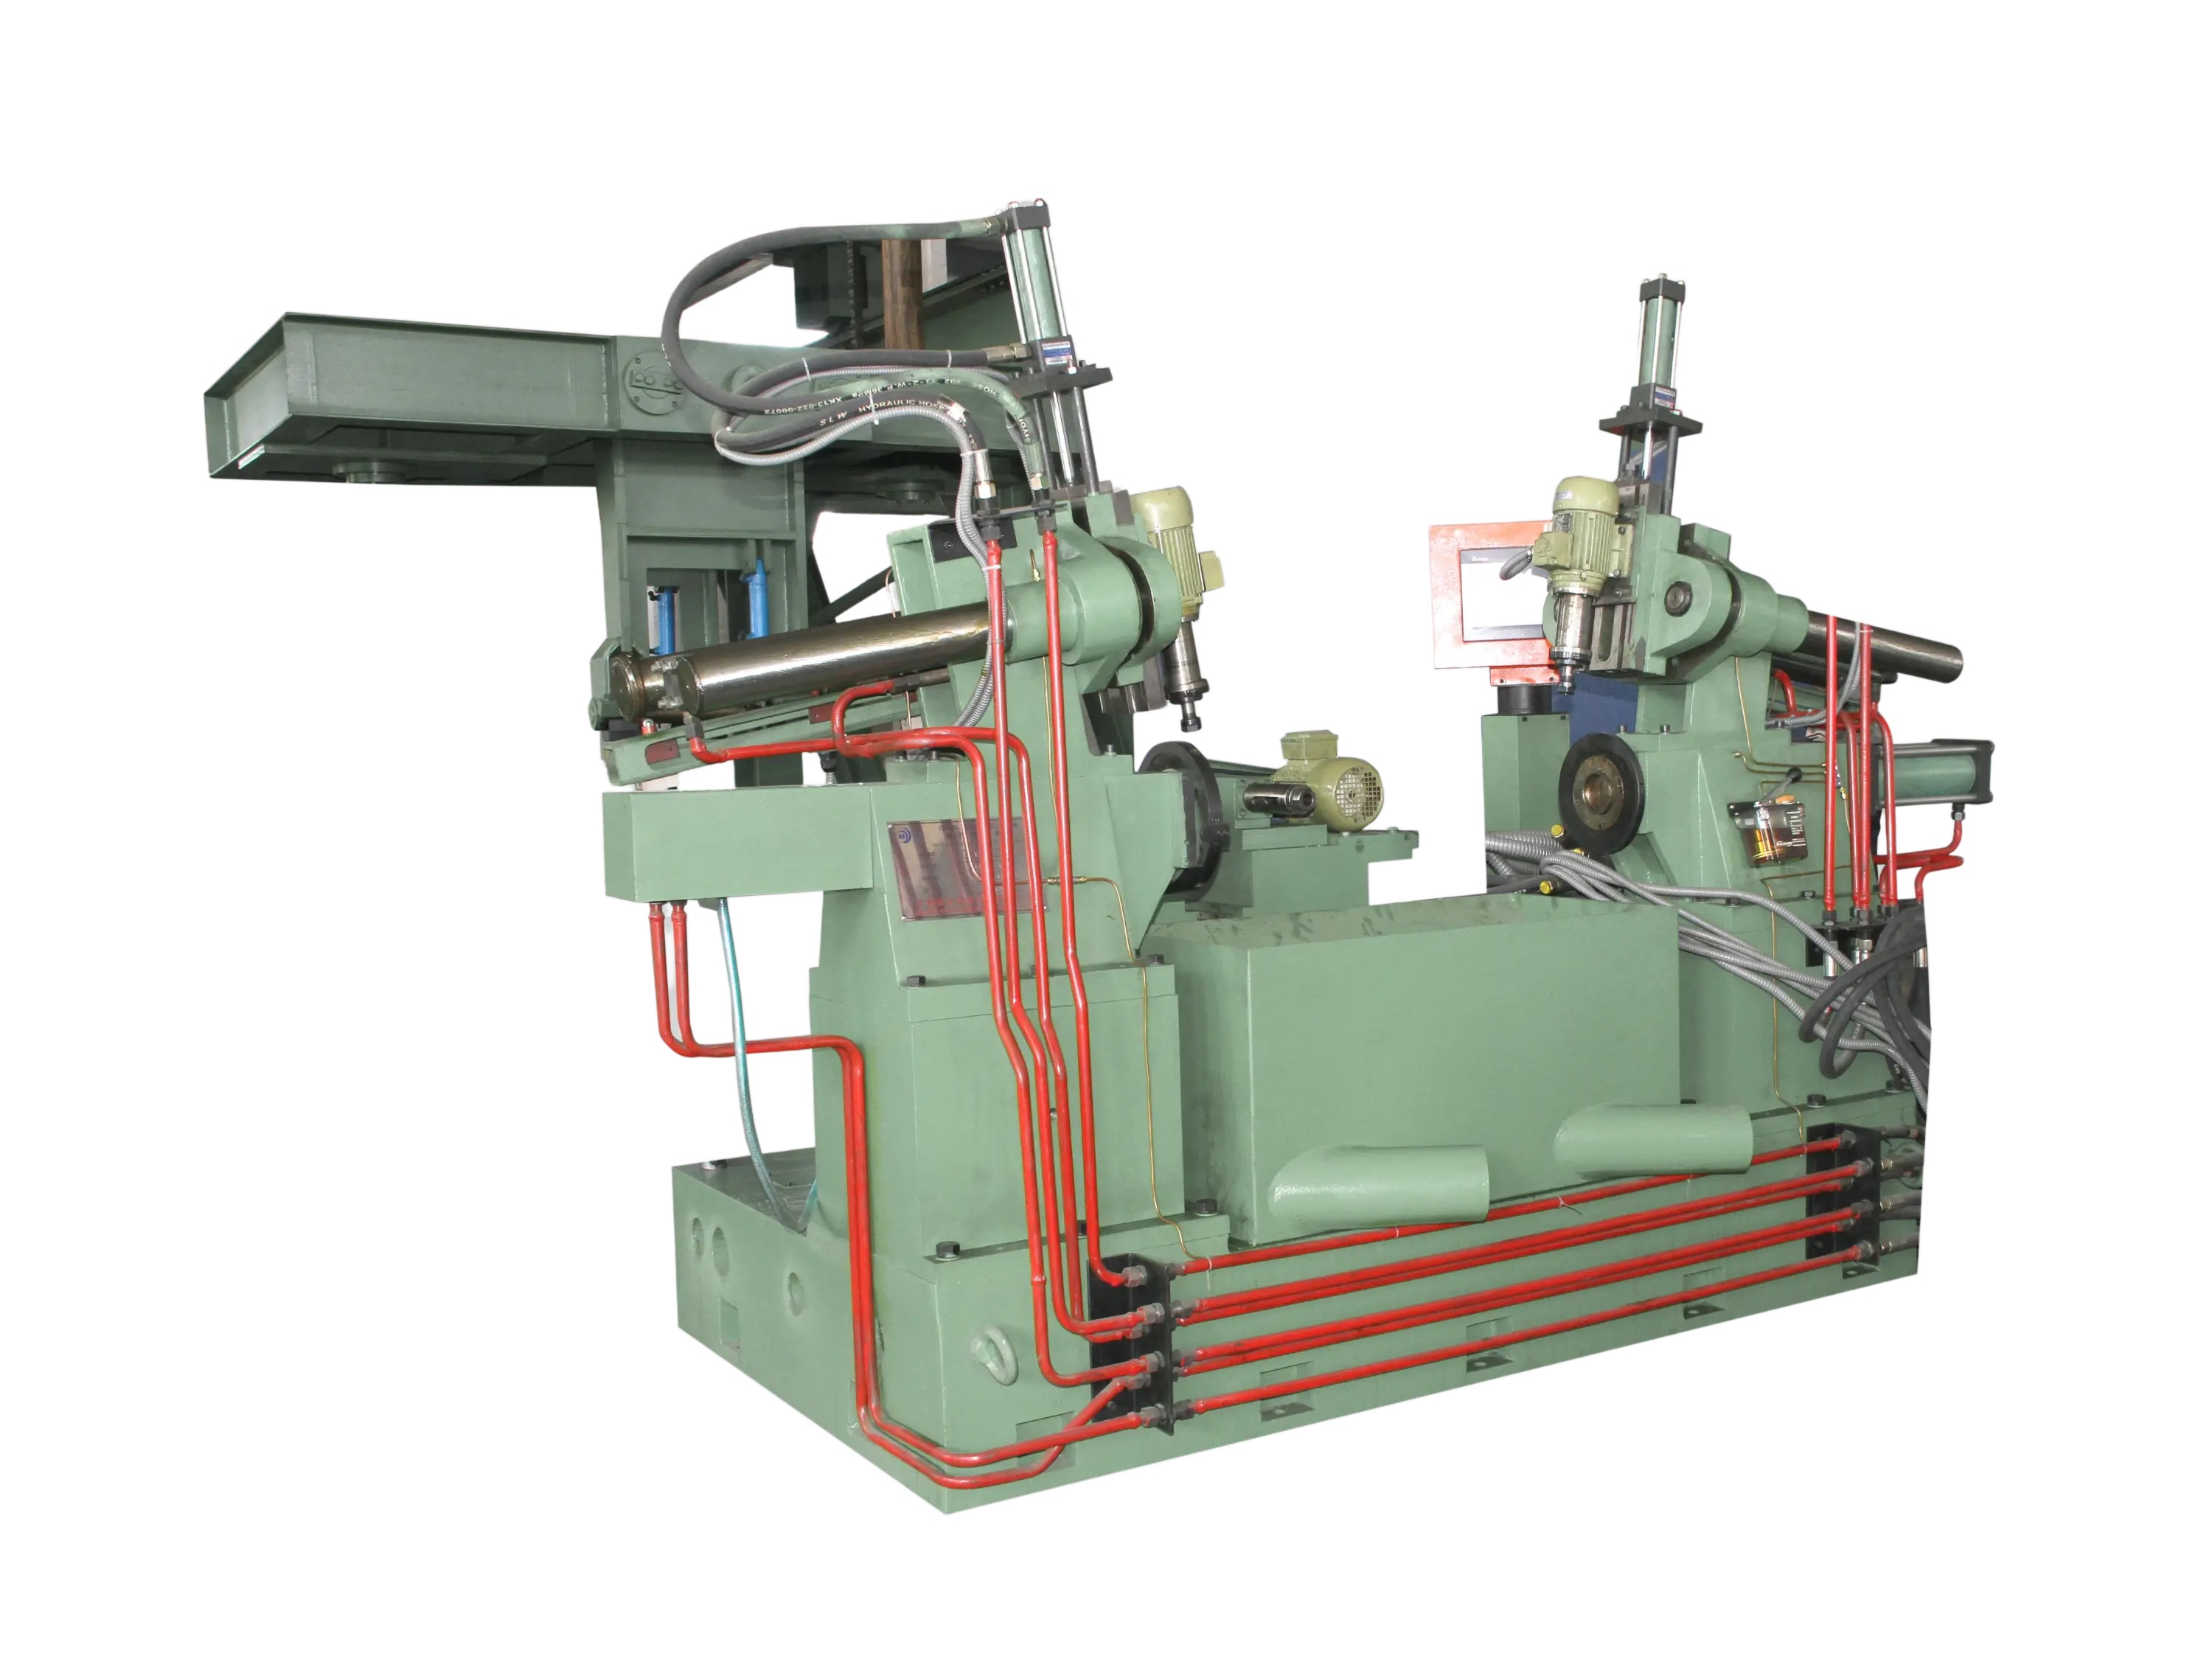
Large graphite electrode nipples need a machined slot for the assembly wrench and a bolt hole for the safety bolt that prevents the joint from loosening during furnace operation. The CGK-28 mills the slot and drills the bolt hole on both ends of the nipple in one clamping, using the centre hole as a shared datum. By combining milling and drilling in one setup, it removes a re-clamping step and keeps the slot and bolt hole in the correct angular and axial relationship to the thread.
Request a Quote →Key Features & Working Principle
Six capabilities that turn separate slotting and drilling operations into one accurate CNC cycle.
Slot Milling + Bolt-Hole Drilling
The machine combines the slot mill and the drill in one cycle, so the handling slot and bolt hole are produced in the same setup.
Double-End Processing
Both ends of the nipple are machined in one clamping, keeping the slot and hole positions rotationally aligned to each other.
Centre-Hole Datum Reference
The nipple is located on its centre hole, so every slot and hole is positioned from the same axis used by upstream and downstream stations.
Full CNC Axis Control
All cutting positions are CNC controlled, eliminating mechanical stops and template-dependent errors from feature placement.
Stepless Spindle Speed
The spindle runs from 200 to 250 rpm with stepless adjustment, letting the operator fine-tune speed for the graphite grade and cutter diameter.
Compact Bed Design
A 4.2 tonne machine body keeps the machine rigid while the compact 2060×1200×1500 mm footprint fits into existing nipple-shop layouts.
Why Choose the CGK-28
Against separate slot mills and drill presses, the CGK-28 wins on feature alignment, handling efficiency and floor space.
One Machine Finishes Two Features
Slot milling and bolt-hole drilling are done in one cycle, removing a transfer step and the stack-up error it introduces.
One Clamping Replaces Two Setups
Double-end processing in one fixture removes a re-clamp, a crane move and the reference shift that often comes with it.
Consistent Feature Placement
CNC coordinates hold the slot depth, width, angle and bolt-hole position from the first piece to the last.
Wide Diameter Range
One machine covers Φ120–Φ431 mm nipple diameters and 177–635 mm lengths, so a nipple shop serves multiple electrode grades.
Reliable Joint Security
Accurate bolt holes and slots ensure the safety bolt and wrench features work as designed in the furnace joint assembly.
Compact Footprint
At 2060×1200×1500 mm, the machine replaces separate slotting and drilling stations with one, freeing floor space.
CGK-28 — Technical Data
Main technical performance indicators from the factory datasheet.
| Parameter | Unit | CGK-28 |
|---|---|---|
| Model | — | CGK-28 |
| Machined nipple diameter | mm | Φ120–Φ431 |
| Machined nipple length | mm | 177–635 |
| Spindle speed | rpm | 200–250 stepless |
| Pulse equivalent | mm/pulse | 0.001 |
| Machine weight | t | 4.2 |
| Overall dimensions | mm | 2060×1200×1500 |
Materials & Industries Served
Designed for carbon plants adding handling slots and bolt holes to graphite electrode nipples after threading and turning.
Frequently Asked Questions
What does the CGK-28 do?
What nipple sizes can the CGK-28 process?
What accuracy does the CGK-28 achieve?
Why combine milling and drilling in one machine?
What control system does the CGK-28 use?
What information is needed for a quotation?
Configure a CGK-28 for Your Nipple Production
Send us your nipple diameter and length range, slot dimensions and position, bolt-hole size, thread standard and pitch, electrode grade, daily throughput target, and workshop layout — including power supply and foundation requirements. Our engineering team will prepare a machine configuration with confirmed specifications and a quotation.
Request a Quote →