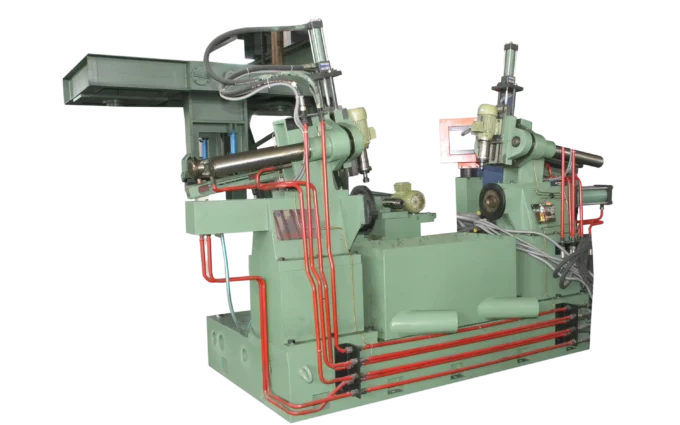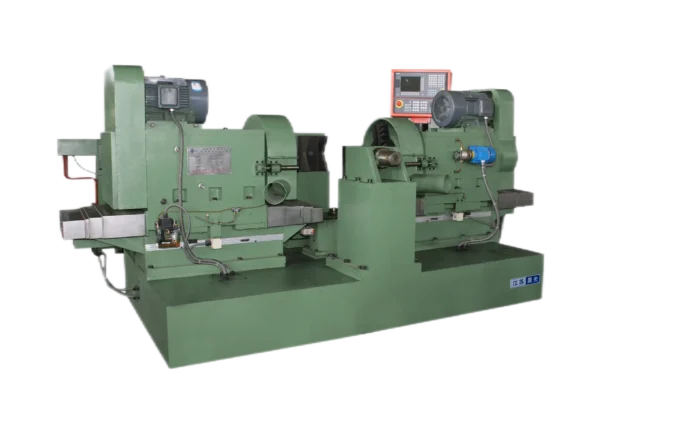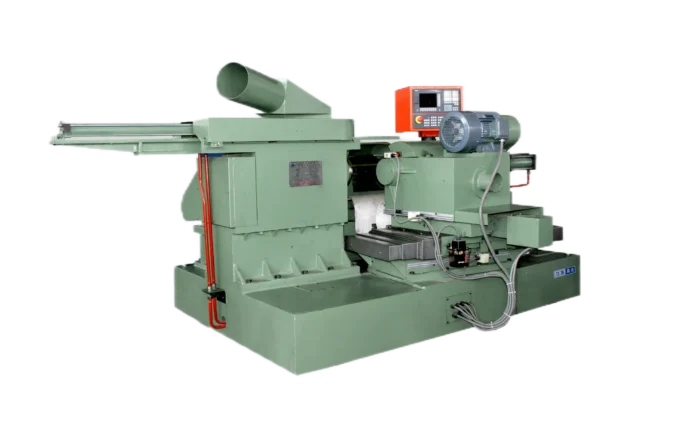
CGK-26 CNC Joint Double Outer Cone Lathe
Both Cones, One Setup, One Taper
The CGK-26 is built for plants machining graphite electrode nipples — turning the external taper that mates with the electrode socket on each end of the connector.
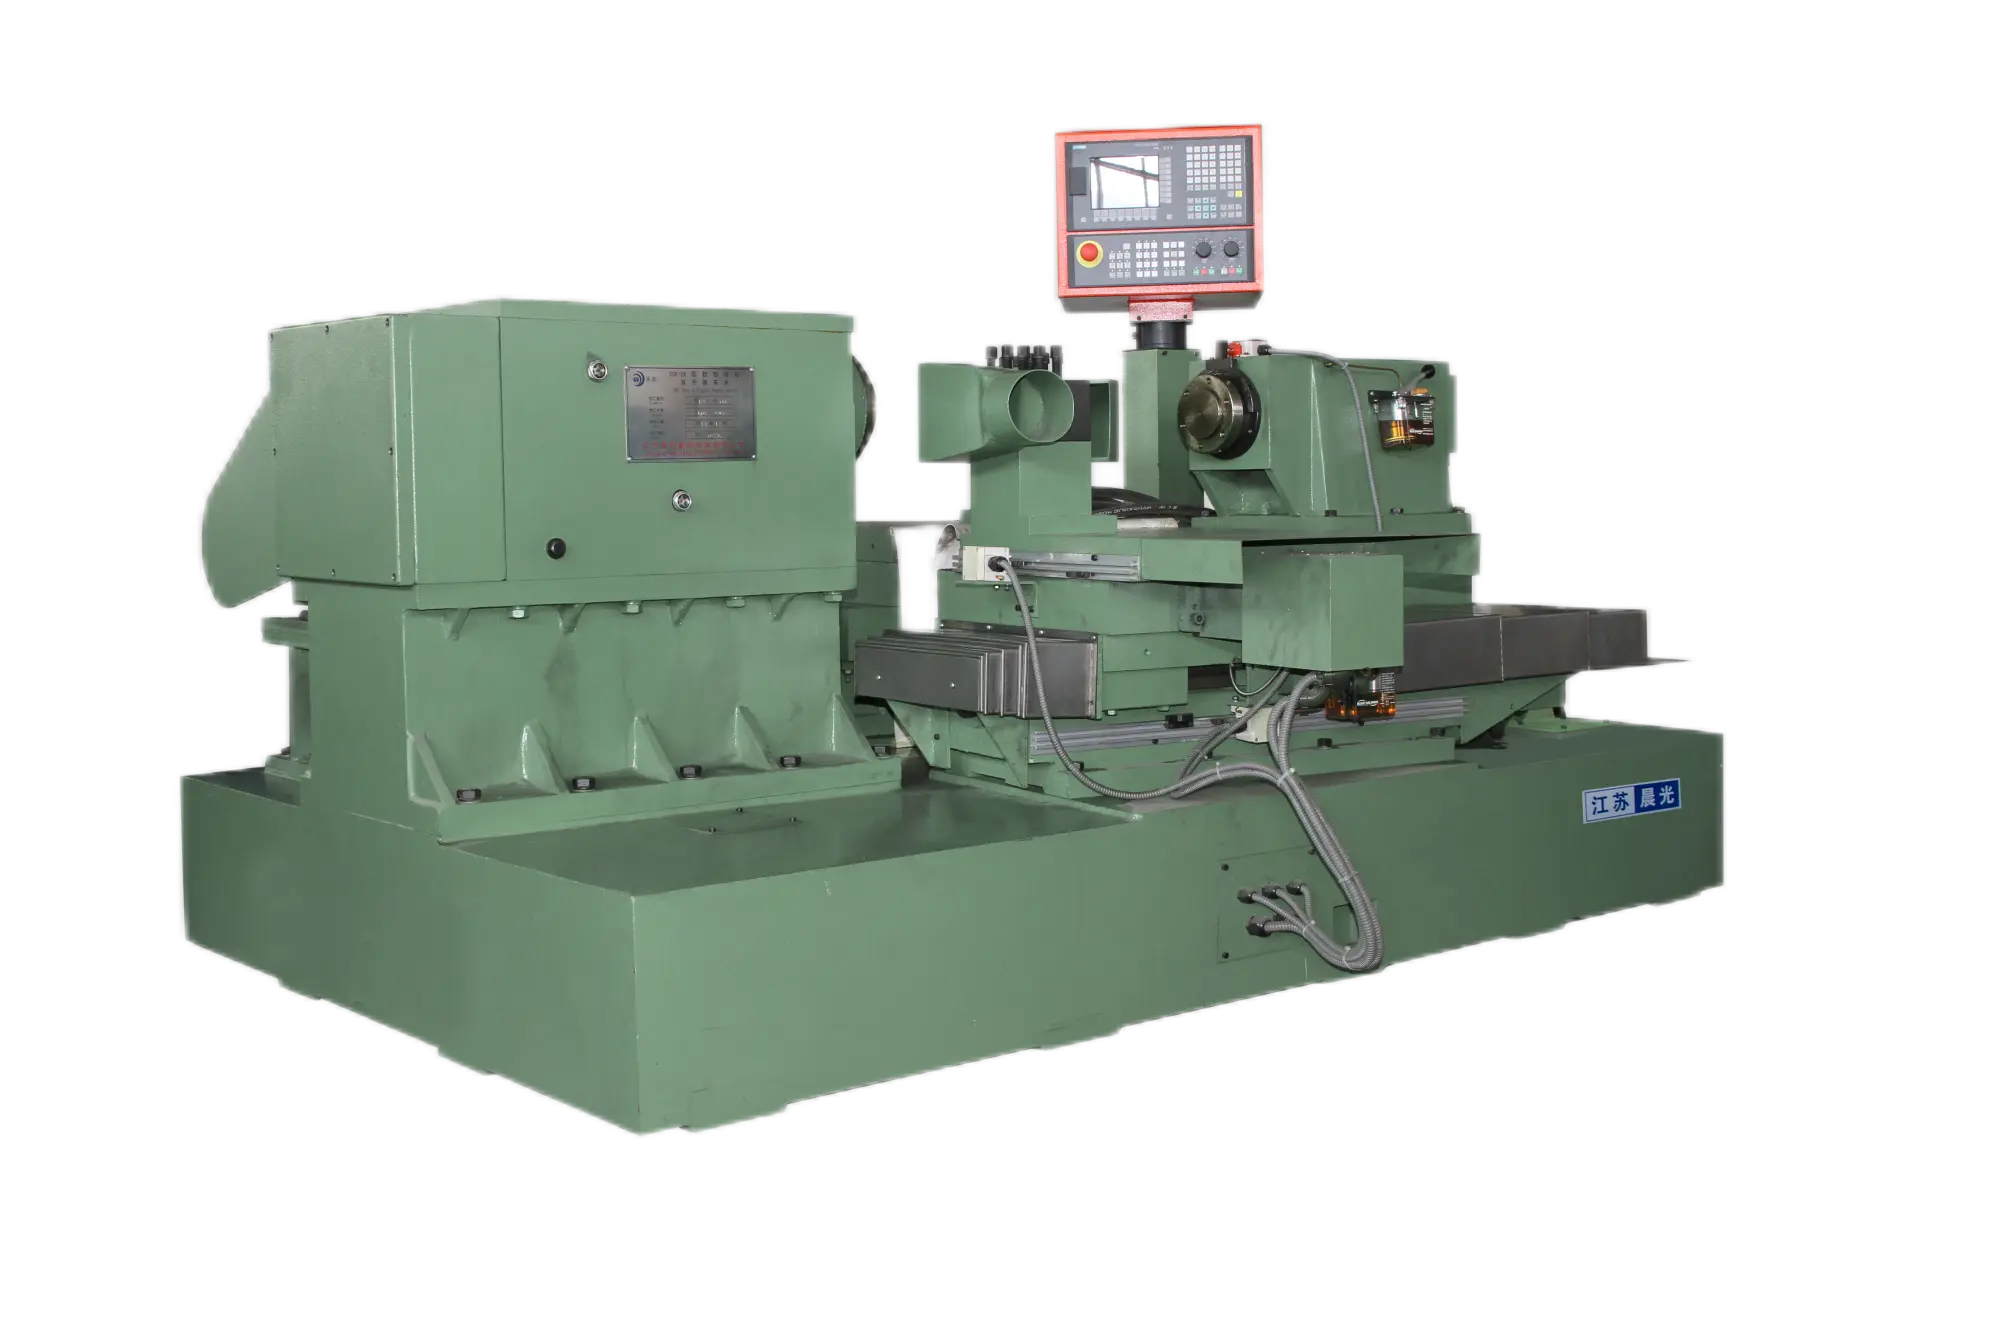
The external cone on a graphite electrode nipple is the sealing surface that seats against the electrode socket. If the two cones on a nipple are not coaxial or their taper angle drifts, the joint leaks current-carrying contact area and runs hot under furnace current. The CGK-26 turns both external cones in one clamping, using the centre hole as a shared datum, so the taper geometry on both ends is referenced to the same axis. That removes the re-clamping error that accumulates when each cone is turned on a separate lathe.
Request a Quote →Key Features & Working Principle
Six capabilities that turn a two-machine cone-turning job into one accurate setup.
Double-End Cone Turning
Both external cones are turned in one clamping, so the two tapers share the same axis and taper ratio from the start.
Centre-Hole Datum Reference
The nipple is located on its centre hole, carrying the datum established by the previous scraping and drilling station straight into cone turning.
Full CNC Axis Control
Every motion axis is CNC controlled, eliminating mechanical transmission-chain error from taper angle and cone profile.
Rigid Cast Bed
A 7.5 tonne machine body absorbs cutting forces during double-end turning, protecting surface finish and taper accuracy.
Wide Taper Program Range
Taper ratios such as 1:3 and 1:6 are stored as part programs, so changeover means a program call rather than a mechanical rebuild.
High-Torque Main Drive
A 7.5 kW main motor drives the turning tool through hard, abrasive graphite grades without stalling or tearing the cone surface.
Why Choose the CGK-26
Against separate lathes for each end, the CGK-26 wins on cone coaxiality, taper consistency and handling efficiency.
Both Cones from One Datum
Turning both cones from the centre hole keeps them coaxial with each other and with the nipple axis — the geometry a furnace joint needs.
One Clamping Replaces Two Setups
Double-end turning in one fixture removes a re-clamp, a crane move and the reference shift that often comes with it.
Consistent Taper Angle
CNC tool paths hold the programmed taper ratio from the first piece to the last, avoiding the operator variability of manual taper turning.
Wide Diameter Range
One machine covers Φ120–Φ431 mm nipple diameters and 177–635 mm lengths, so a nipple shop serves multiple electrode grades.
Smooth Sealing Surface
A rigid bed and controlled CNC feed produce the smooth cone surface that seats cleanly against the electrode socket.
Compact Footprint
At 2430×1600×1500 mm, the machine replaces two standalone lathes with one, freeing floor space in a busy nipple shop.
CGK-26 — Technical Data
Main technical performance indicators from the factory datasheet.
| Parameter | Unit | CGK-26 |
|---|---|---|
| Model | — | CGK-26 |
| Machined nipple diameter | mm | Φ120–Φ431 |
| Machined nipple length | mm | 177–635 |
| Main motor power | kW | 7.5 |
| Spindle speed | rpm | 230 |
| Pulse equivalent | mm/pulse | 0.001 |
| Length error | mm | 0.1 |
| Machine weight | t | 7.5 |
| Overall dimensions | mm | 2430×1600×1500 |
Materials & Industries Served
Designed for carbon plants turning the external taper on graphite electrode nipples before final threading and inspection.
Frequently Asked Questions
What does the CGK-26 do?
What nipple sizes can the CGK-26 process?
What accuracy does the CGK-26 achieve?
Why turn both cones in one setup?
What control system does the CGK-26 use?
What information is needed for a quotation?
Configure a CGK-26 for Your Nipple Production
Send us your nipple diameter and length range, taper ratio, thread standard and pitch, electrode grade, daily throughput target, and workshop layout — including power supply and foundation requirements. Our engineering team will prepare a machine configuration with confirmed specifications and a quotation.
Request a Quote →